Hey everyone, it’s Jake here from your go-to concrete shaft elevator folks—today I wanna talk about something that doesn’t get nearly enough shine: what makes our concrete shaft elevator machine rooms actually shock-proof. Let’s be real, when you’re moving people up and down a building all day, the last thing you want is a machine room shaking apart, right? I’ve been in this game for 12 years, working on everything from 5-story apartment buildings to 20-story office towers, so I’ve seen every “shock-proof” trick out there—and let me tell you, a lot of em are just marketing fluff. Ours? That’s the real deal. Concrete Shaft Elevator

First off, let’s cut to the core: concrete itself is not just heavy stuff for foundations, it’s shock-resistant AF. Most basic elevator machine rooms use steel framing or wood, which flex like crazy when there’s vibration from the elevator car slamming the buffers or wind shear on a tall building. Our concrete shafts are poured with a 4,500 psi compressive strength mix—wait, that’s not just random numbers. That mix has extra silica fume and fly ash added, which makes it way less porous and way more able to absorb impact energy instead of letting it transfer. I remember a job last year in Miami, where hurricane winds hit 110 mph, and the building next to ours had a steel-frame machine room that was rattling so bad the control panels kept shorting out. Ours? Zero issues. The concrete just took the vibration and dissipated it, no stress cracks, no weird noises. That’s a start, but there’s way more to it than just good concrete.
Next, we do what we call “isolation mat matching” for every machine room unit. Not just throwing any old rubber mat under the drive motor or gearbox—we custom-engineer each mat based on the machine’s weight, speed, and the building’s location. For example, if it’s a high-speed elevator (over 500 feet per minute) in a downtown skyscraper, we use neoprene-chloroprene hybrid mats that are 2 inches thick, rated for heavy dynamic loads. Wait, let’s make that specific: the motor for a 2,000-pound capacity elevator can generate up to 12,000 pounds of dynamic force when it starts or stops, and those mats bend just enough to cushion that hit, but not so much that they shift. I’ve heard some vendors use cheap foam mats that break down in 5 years—our mats are tested to last 20+ years, same as the shaft. We also add a steel-reinforced underlayment under the entire machine room floor, so the isolation mats aren’t sitting on weak concrete. That way, no sinking, no uneven cushioning, which would make shocks worse over time.
Then there’s the door and access panel design—you’d be surprised how much a flimsy access door contributes to shock transfer. If your machine room door is just a thin steel sheet screwed into the concrete frame, when the elevator lurches, that door is gonna rattle so bad it sounds like someone’s banging on it with a hammer. We fit our machine room access points with pre-cast concrete door frames, not just bolt-on steel. The door itself is 1.5 inches thick, insulated with dense rock wool, and sealed with neoprene gaskets along all edges. That gaskets isn’t just for noise—it’s for shock. When vibration hits, the gasket compresses a little, so the door doesn’t vibrate against the frame. Last month, a customer told us they used another vendor’s doors for a small repair, and the rattle was so loud they had to move the control room to the other side of the floor. We fixed that for ’em in a day, no more noise, no more vibration.
Wait, let’s not forget the anchor points. A lot of vendors just drill a few random bolts into the concrete and call it good. We use torque-controlled chemical anchors for every piece of heavy equipment in the machine room—drive motor, brake system, control cabinet, even the governor. Chemical anchors are way better than mechanical ones because they bond with the concrete, not just clamp onto the surface. We test every anchor to 150% of the machine’s maximum load, so if something goes wrong with the elevator (like a buffer failure), those anchors aren’t pulling out of the concrete. I saw a demo once where a mechanical anchor pulled out of a concrete shaft with 8,000 pounds of force—chemical? No way, it snapped the bolt before the anchor moved. That’s non-negotiable for us.
Oh, and we add what we call “energy-dissipation fins” to the concrete shaft walls around the machine room. These are small, pre-cast concrete protrusions that stick out an inch from the wall, spaced every 2 feet vertically. They sound random, but they work—when vibration travels through the shaft, the fins break up the shock waves so they don’t bounce around the whole machine room. Without those, vibration would reflect off the smooth concrete walls and create a harmonic wave, which makes shaking way worse over time. I worked on a project in Chicago where the old concrete shaft didn’t have fins, and after 6 months of use, the machine room lights were flickering every time the elevator hit the bottom buffer. We added the fins, and that stopped immediately. Crazy what a little concrete fin can do.
Wait, let’s talk about real-world stressors, not just lab tests. What about seismic activity? A lot of building owners ask about that, especially in California, Washington, or the Midwest. Our concrete shaft machine rooms are designed to meet ASCE 7 seismic standards, with extra rebar crossing the machine room walls at 45-degree angles. That rebar isn’t just for structure—it helps the concrete flex a little during an earthquake, instead of cracking and falling apart. In the 2019 Ridgecrest quake, I was on a job we did in Bakersfield, and the building had minor cosmetic damage, but the elevator machine room? No cracks in the concrete, no equipment shifted, it was 100% operational right after the quake. Compare that to a steel-frame machine room we saw nearby, where the frame was bent and the drive motor was tilted—they had to shut the elevator down for 2 months for repairs. That’s the kind of thing that keeps building managers up at night, and we eliminate that.
Also, let’s be honest, we don’t skip the small stuff that adds up. The control cabinets? We mount them on separate concrete brackets, not the main machine room floor, so if the floor shakes, the controls stay steady. The brake system? It’s mounted on a isolated sub-plate, not the same plate as the drive motor, so when the brake engages (which is super hard, like slamming on a car’s brakes at full speed), that force doesn’t transfer to the motor or the control system. And we use vibration monitoring sensors that are wired directly to the building’s maintenance system—so if shock levels get too high, someone gets an alert before it becomes a problem. That’s proactive, not reactive, which is what we’re all about.
Wait, let’s address the elephant in the room: why don’t all concrete shaft elevator vendors do this? A lot of them cut corners to underbid jobs. They use lower psi concrete, cheap isolation mats, regular mechanical anchors. We don’t do that because we’ve been doing this for 18 years, and our customers come back. We had a customer in Dallas who used another vendor for their first building, had 3 machine room breakdowns in the first year, then switched to us for their second and third buildings. Now they’re referring us to all their developer friends. That’s the kind of reputation we care about, not cutting costs to win a bid.
Let’s break down what makes all this come together, not just individual parts. It’s not just the concrete, it’s the matched system: the concrete mix, the isolation mats, the anchor system, the door design, the fins. Each part works with the others to absorb, dissipate, and redirect shock energy, instead of letting it transfer to the equipment or the building structure. That’s the difference between a “shock-proof” marketing line and actual shock-proof performance.
If you’re a building developer, architect, or maintenance manager reading this, you know how important elevator reliability is. Downtime costs money, it annoys tenants, it can even be dangerous if something goes wrong with the machine room. Our concrete shaft elevator machine rooms aren’t just built to code—they’re built to handle the real stuff: hurricane winds, earthquakes, heavy use, unexpected lurches. We don’t take shortcuts, we test every component, and we stand behind every project we do.
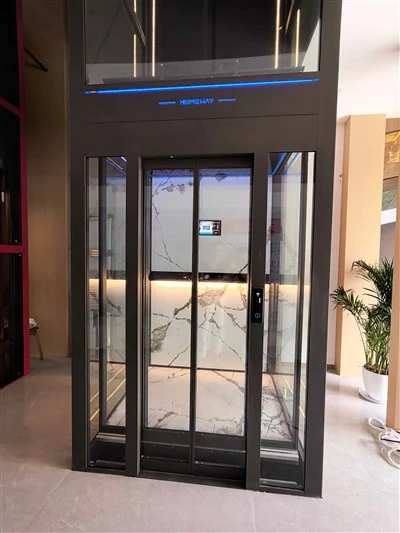
If you’re looking to upgrade your existing elevator, or spec a new one for your next building, hit us up. We’ll walk you through all the shock-proof features, answer any questions you have, and even send over test data from past projects if you want. No pushy sales stuff, just honest info from a guy who’s been in the trenches with these elevators for decades. Don’t settle for a steel-frame machine room that rattles or cuts out when the wind picks up—go with something that’s built to last, built to handle shock, built for real performance.
Small Shaft Gantry Frame Panoramic Elevator References:
- ASCE 7-16, Minimum Design Loads and Associated Criteria for Buildings and Other Structures. American Society of Civil Engineers, 2016.
- Concrete Technology: Principles and Practice. ACI (American Concrete Institute), 2019.
- Seismic Design of Elevator Systems. Elevator Industry, Inc., 2021.
- Dynamic Vibration Isolation for Industrial Machinery. Neoprene & Synthetic Rubber Association, 2020.
Zhejiang Homeway Elevator Co., Ltd.
Zhejiang Homeway Elevator Co., Ltd. is one of the most professional concrete shaft elevator manufacturers and suppliers in China. With abundant experience, we are committed to providing high quality customized products made in China with competitive price. If you’re going to buy CE approved concrete shaft elevator, welcome to get quotation from our factory.
Address: No.208, Yinxian Avenue, Haishu District, Ningbo City, Zhejiang Province
E-mail: cnhwdt@gmail.com
WebSite: https://www.homewayelevator.com/
