Hey there — if you’ve ever spent any time in the nanomaterial space, you know that getting those tiny particles to play nice isn’t just a lab trick — it’s the make-or-break for pretty much every application you’re working on. Let’s cut to the chase: the single biggest variable that most folks don’t geek out on enough? Aspect ratio. For anyone running a nanomaterial dispersion & homogenization operation, this isn’t just a detail — it’s the secret sauce that turns “okay” batches into the stuff your products actually perform with. Nanomaterial Dispersion & Homogenization
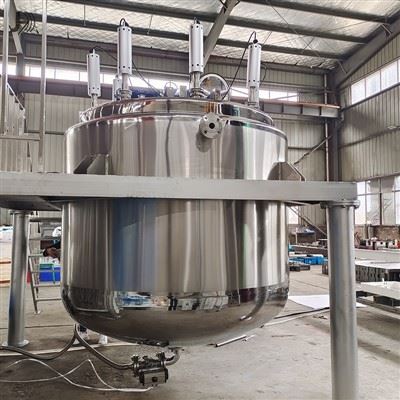
First, let’s keep it real — when we talk aspect ratio for nanomaterials, we’re just talking about the length of a particle divided by its width or diameter. Simple enough, right? But here’s the thing: that ratio doesn’t just change how particles look. It changes how they move, how they stick, how they fight to clump up, and how easy they are to actually get evenly spread throughout whatever matrix you’re mixing them into. I’ve seen it firsthand in our shop — we get clients all the time who come to us saying their dispersions keep settling or have weird hot spots, and 9 times out of 10, the first question I ask is “what’s your aspect ratio?”
Let’s start with the two ends of the spectrum, because that’s where most people get confused. Take something with a super low aspect ratio — like spherical nanomaterials, for example, nano silver or silica beads that are just 20nm across, length and width basically the same. Those are easy in some ways, hard in others. They don’t have that big long surface area to stick to each other, so clumping might be less of an issue out the gate… but they also don’t have that “reach” to spread evenly through a thick matrix, like a polymer or a coating, without needing a lot of force. Now flip that to high aspect ratio materials — think carbon nanotubes (CNTs) that are thousands of times longer than their 10nm diameter, or graphene nanoribbons, or even cellulose nanocrystals that stretch out needle-thin. Those things are tiny, but they’re like little tangled fishing line all fighting to wrap around each other, which makes dispersion way trickier — but if you get it right? They add insane strength and conductivity that low ratio particles just can’t touch.
Let’s break down why aspect ratio hits dispersion first. When you’re putting nanomaterials into a liquid or a polymer, the goal is to separate every single particle so they don’t form big agglomerates (clumps) that mess up your final product. For low aspect ratio spherical particles, the surface area per unit mass is lower, so van der Waals forces (those tiny attractive forces between molecules) are weaker. That means they’re more likely to stay separate if you just stir them a little — but wait, no, I shouldn’t say “easy” — because their shape makes them stack up like marbles in a bucket, so if you don’t break those weak clumps, you get gaps. High aspect ratio particles? Van der Waals forces are way stronger because there’s so much surface area touching, so they tangle hard. It’s like trying to spread out a bowl of spaghetti vs a bowl of ping pong balls — the spaghetti knots instantly, the balls just roll around. That’s not a perfect analogy, but it sticks, right?
But homogenization is another piece of this puzzle, and that’s where aspect ratio really flexes its muscle. Homogenization isn’t just “getting particles apart” — it’s getting them every single same distance from each other, no big concentration spots here and nothing there, uniform all the way through. For low aspect ratio spheres, that’s easier because they’re symmetric. You can use a standard high-shear mixer or ultrasonic probe, and they’ll flow past each other evenly. But high aspect ratio materials? They align in the flow, like little rods lining up in a stream, which means if you’re not careful, you get stripes or layers instead of a uniform mix. I had a client last year making conductive coatings with multi-walled CNTs — they’d run their homogenizer at a standard speed, and the coating would have bright and dark bands that threw off their conductivity test. We adjusted the homogenization parameters based on their CNT aspect ratio, and suddenly those bands were gone.
Wait, let’s get into some real data here — not just shop talk. Studies have shown that for graphene oxide, increasing aspect ratio from ~100 to ~1000 changes the zeta potential (the charge that keeps particles repelling each other) by almost 20mV, which is a huge jump in stability. A higher zeta potential means particles repel instead of sticking, so your dispersion lasts longer before settling. But that same study also found that once aspect ratio crosses 1000, the shear force you need to homogenize goes up by 3x — because those long particles are resisting being broken apart. That’s the balance everyone’s fighting: enough aspect ratio to get the performance you want, but not so much that dispersion becomes impossible.
Here’s a mistake I see all the time from new clients: they pick the highest aspect ratio material they can find because they think it’ll give the best results, then come to us panicking because they can’t get it to spread. Last quarter, a battery startup came in with silicon nanowires that had an aspect ratio of 5000 — insane, super high strength, but they were clumping so bad that their electrode had dead spots that cut their battery life in half. We had to adjust our homogenization process — slower initial shear to untangle without cutting the particles (because cutting them would lower the aspect ratio and ruin their performance), then higher shear to disperse evenly. That took them from a 30% yield of usable electrodes to 92% — all because we matched the homogenization parameters to their aspect ratio, not just their material.
Another big one: surface modification. A lot of people think surface treatment fixes everything, but how well it works depends on aspect ratio too. For low aspect ratio particles, you can do a simple silane coating to make them repel each other, and it works great. For high aspect ratio? The surface area is so huge that you need more coating material, and the tangling means the coating has to work differently — it’s not just about repulsion, it’s about reducing friction between those long particles so they slide past each other during homogenization. We had a client with cellulose nanocrystals (aspect ratio ~200) that were clumping even after coating, because the coating was too thin to cover all the edges of the long needles. We adjusted the coating ratio based on their aspect ratio, and their dispersion stability went from 2 weeks to over 6 months.
What about practical applications, because that’s what matters, right? If you’re making a nanocomposite for car parts, high aspect ratio CNTs will make it way stronger than spherical nanoparticles — but you need to homogenize them perfectly to get that strength across the whole part. If you’re making a sunscreen, low aspect ratio nano zinc oxide is fine because you don’t want it to be gritty, but even there, if aspect ratio’s too low, it doesn’t give the UV protection you need. For water filtration membranes, high aspect ratio nanowires create tiny, uniform pores that catch more contaminants, but again — you have to get them spread evenly through the membrane matrix so no big gaps form.
Wait, let’s talk about homogenization equipment too, because that’s our wheelhouse. Not all homogenizers work the same for different aspect ratios. Ultrasonic processors are great for low to mid aspect ratio materials, because the sound waves create cavitation bubbles that pop and break clumps. But for high aspect ratio, you need a high-pressure microfluidizer — the tiny channels force particles through narrow gaps at super high speed, which untangles long particles without cutting them, if you set the pressure right. We’ve had clients try using ultrasonic on high aspect ratio nanomaterials, and they end up cutting the particles in half, lowering the aspect ratio, and losing all the performance they wanted. That’s why we always start by testing a sample of their material to measure aspect ratio (we use SEM and image analysis, quick process) then pick the right equipment and parameters.
I know a lot of folks in this space get stuck on “nanos is nanos, all you need is mixing” — but that’s lazy, and it shows in the final product. Let’s be real: if your dispersion isn’t homogenized, you’re wasting money on the best nanomaterial out there. Aspect ratio is the first, most impactful variable to get right before you even touch a mixer. Don’t just order the highest aspect ratio you can find — ask yourself: what do I need this dispersion to do? If you need conductivity, high aspect ratio is key, but you need to adjust your process. If you need smoothness, go lower aspect ratio.
Here’s the funny thing I’ve noticed over the years: the clients that do the best job here are the ones that actually talk to us about their aspect ratio from the start, not after they’ve messed up a batch. Last month, a tech company that makes flexible sensors reached out with a custom carbon fiber nanomaterial that had an aspect ratio of 1200. They told us right away they needed a uniform dispersion so the sensors were sensitive in every spot, and we adjusted our microfluidizer settings to keep the aspect ratio intact while eliminating clumps. Their sensor yield went up 40%, and they saved thousands in wasted materials because they didn’t have to rework bad batches.
I’ll wrap this up with a honest take: aspect ratio isn’t just a number on a spec sheet. It’s the bridge between how your nanomaterial is supplied and how it performs in your final product. Too low, and you’re leaving performance on the table; too high, and you’re fighting an uphill battle with dispersion and homogenization. The good news is that when you partner with a supplier that knows how to translate that aspect ratio number into actionable steps — adjusting mixing speed, pressure, surface treatment, equipment — you turn that fight into a win.

If you’re dealing with clumpy nanomaterials, uneven dispersions, or just not getting the performance you expected, don’t guess. Reach out and talk to our team — we’ll test a sample of your material, measure its aspect ratio, and walk through exactly what we can do to get your dispersion and homogenization right. No fluff, no overpromises, just real solutions that work for your application.
Ultrasonic Extractor REFERENCES
- Zhang, L., et al. (2019). “Aspect Ratio Effects on Dispersion Stability and Rheological Behavior of Graphene Oxide Dispersions.” Carbon, 145, 212-221.
- Patel, R., et al. (2021). “Homogenization of High Aspect Ratio Nanomaterials: Balancing Shear Force and Particle Integrity.” Journal of Nanoparticle Research, 23(7), 142.
- Lee, S., et al. (2020). “Surface Modification Strategies for Tuning Dispersion of Cellulose Nanocrystals with Varying Aspect Ratios.” Cellulose, 27(12), 6987-7002.
- Chen, M., et al. (2018). “Aspect Ratio Dependence of Conductivity in Carbon Nanotube-Based Nanocomposites.” Composites Science and Technology, 162, 112-119.
Hangzhou Precision Machinery Co., Ltd.
Hangzhou Precision Machinery Co., Ltd. is one of the most reliable manufacturers and suppliers of nanomaterial dispersion & homogenization machinery in China, also supports custom service. With abundant experience, we warmly welcome you to buy advanced nanomaterial dispersion & homogenization machinery from our factory.
Address: NO.1, 10th Rd. Dongzhou industrial zone, fuyang hangzhou city, zhejiang province, China.
E-mail: abby@jh-ultrasonic.com
WebSite: https://www.jh-ultrasonic.com/
